If you’ve walked the floor of any metal fabrication or aerospace machine shop, you’ve probably heard the question thrown around between machinists and production managers: Can this CNC drilling machine I’ve got (or am looking at) actually do both through-hole drilling and blind-hole drilling? For years, I heard this debate on a near-daily basis when I was on the floor testing our own CNC drilling units, and now that I’m a CNC drilling machine supplier who gets calls about this exact topic every week, I can tell you it’s not a yes/no answer—it’s a “yes, but you have to know how it works, and which small details make or break the job.” CNC Drilling Machine

Let’s start with the basics that most people skip over. First, what’s the difference between a through-hole and a blind hole, anyway? A through-hole goes all the way through a workpiece—think of a bracket that needs a bolt hole passing from one side to the other to connect to a mating part. A blind hole stops short of the other side, leaving a solid “land” of material at the bottom; that’s common for things like mounting holes for a bearing housing, where you don’t want the bolt to poke through the back and rub on internal parts. At its core, both are just cylindrical holes made by removing material with a rotating tool, right? So why would a CNC drilling machine not handle both?
The short answer is: Most CNC drilling machines are designed for both. But before we go further, I should clarify that I’m not talking about the low-cost, single-spindle benchtop units some hobbyists use for small projects. I’m referring to the industrial CNC drilling machines we supply—units built for production runs, consistent tolerances, and repeatability, which is what 90% of our commercial and industrial clients are buying for. Let’s break down how each hole type works with these machines, and where a lot of the confusion comes in.
First, through-hole drilling with a CNC drilling machine. The process here is straightforward, in theory: you program the machine to move the drill bit straight down at a set RPM and feed rate, until it travels the full thickness of the workpiece. But what many people don’t realize is that CNC automation is what makes through-hole drilling reliable, even for high-volume jobs. A manual drill press might let you drill through a 1-inch steel plate, but you’ll have to adjust pressure to avoid wandering, or cleanup the burr that’s left on the exit side. A CNC drilling machine does this by locking in a consistent axis path—no operator-induced wobble—and often adds built-in features like peck drilling to clear chips as the bit goes, which prevents overheating and breaks. For example, our mid-sized multi-spindle CNC drilling line has a pre-programmed peck cycle that adjusts depth by 0.1 inches every time the bit retracts, pushing metal chips out of the flutes so the bit doesn’t bind. For through-holes, this is game-changing, especially on thick workpieces or hard metals like aluminum or stainless steel.
Where blind-hole drilling gets trickier is in the details—specifically, depth accuracy, chip management, and avoiding “bottoming out” too hard. A blind hole requires the machine to stop exactly at the programmed depth, within a tolerance of a few thousandths of an inch, so you don’t accidentally drill through and create a partial through-hole that ruins the part. That’s where CNC really shines: manual methods use a depth stop, which wears out over time and is hard to adjust for varying part thicknesses or bit wear. A CNC drilling machine uses a linear encoder on the Z-axis (the axis that moves up and down, for those who don’t work in CNC every day) that tracks position to within 0.0005 inches. When the drill reaches the blind hole’s programmed depth, it automatically retracts—no more guessing.
But let’s get to the part that trips up a lot of new users: even though both hole types are possible, you have to adjust your setup and program based on which you’re making. Let’s talk about common mistakes I see clients make when switching between through and blind holes on the same machine. First, for through-holes, you have to account for “exit travel”—that’s the distance the bit will travel past the bottom of the workpiece to fully break through, without slamming into the machine’s workholding or the table. A manual drill press operator would eyeball that, but a CNC drill lets you program that extra distance, and our machines even have a built-in collision avoidance feature that lets you set a “no-go” zone on the table so the bit never hits anything. For blind holes, that extra exit travel doesn’t exist—instead, you have to set a “clearance” at the bottom of the hole, meaning the bit stops short of a full contact with the material, leaving a small land. Wait, no—actually, some jobs do require a flat bottom on a blind hole, right? That’s called a “bottoming blind hole,” and that’s a slightly different programming step. For that, you slow the feed rate to almost a crawl in the last 0.05 inches, so the bit cuts cleanly without gouging or drilling past the intended depth.
Another big factor: tooling. I can’t tell you how many times a client will call me, frustrated, saying their CNC drilling machine won’t make good blind holes, and it turns out they’re using a general-purpose twist drill bit made for through-holes. Twist drills have a pointed tip, and when you stop them in a blind hole, that point can leave a small “dimple” or uneven bottom, which is fine for through-holes where that dimple will be on the exit side, but not for blind holes where you need a flat surface for a bearing or fastener. For blind holes, we recommend using a spotting drill to create a pilot hole first, then a flat-bottom drill (also called a center drill or a counterbore drill, depending on the size) that cuts a uniform bottom. Our clients who make automotive parts, for example, will switch between through-holes for frame brackets and blind holes for engine mounts on the same CNC drilling line, and the tool change is fully automated—no manual swapping, just a quick programmed call to the tool changer.
Wait, but is there any limit? Are there hole sizes or materials where a CNC drilling machine can’t do both? Absolutely. Let’s be realistic. If you’re drilling a 1-inch deep blind hole in a block of titanium, a standard 3-axis CNC drilling machine can handle that, but you’ll need to adjust RPM and feed rate to prevent bit wear. If you’re drilling a 1-foot deep through-hole in a 2-foot thick steel plate, that’s a job for a heavy-duty gantry-type CNC drilling machine, not a small benchtop unit. But for 95% of the jobs our clients do—from electronics enclosures with small fastener holes to construction brackets with large mounting holes—the industrial CNC drilling machines we supply handle both hole types without a hitch. The confusion usually comes from people mixing up CNC drilling machines with other CNC tools, like milling machines. A lot of people think, “Well, a mill can do holes, so a drill must work the same,” but mills are for contouring and shaping, while CNC drilling machines are purpose-built for high-volume, accurate hole making, with specialized controls and axes that make through and blind holes seamless.
Let’s talk about a real example, because theory is great, but actual shop floor experience is what matters. Last year, we worked with a aerospace parts manufacturer that was struggling with their old set of manual drill presses, which were making too many scrap parts: blind holes that were either too deep (ruining the part) or too shallow (so bolts wouldn’t seat properly) and through-holes that had inconsistent exit burrs, requiring extra finishing work. They invested in two of our 12-spindle CNC drilling lines, and now they run batches of parts that require both hole types without stopping. For their landing gear brackets, they drill through-holes to connect the bracket to the fuselage, programming 0.2 inches of exit travel on the Z-axis, and the machine automatically deburrs the exit side in the same cycle. For their actuator mounts, which have blind holes that need to hold precision bearings, they switch the tool to a flat-bottom drill, adjust the feed rate in the last 0.03 inches of the program, and the linear encoder ensures the depth is within 0.001 inches every time. Since installing the machines, their scrap rate for these parts dropped by 78%, and their production time per batch was cut in half. That’s the proof right there: a CNC drilling machine isn’t limited to one hole type—it’s built for both.
Another common myth: you need a separate CNC drilling machine for through holes and another for blind holes. I hear this all the time from new production managers who are trying to draw up budgets for new equipment. Let’s debunk that. The only time you’d need a dedicated machine is if you’re running extremely specialized, one-of-a-kind parts, or if you’re drilling holes so deep or with such tight tolerances that even a well-built standard CNC drill can’t keep up. For most high-volume production runs, one CNC drilling machine can handle both, and even mix them on the same part. Our software lets users program multiple hole types in a single job—you can have five through-holes on one side of a workpiece, and three blind holes on the other, all in one continuous cycle, no manual intervention.
What about the technology side that makes this possible? Let’s get into the nuts and bolts (pun intended) for anyone who wants to understand why this works. A CNC drilling machine has three primary axes: X, Y, and Z. X and Y move the workpiece (or the spindle head) horizontally to position the drill over the correct spot, and Z moves the spindle up and down to drill. For a through-hole, the Z-axis travels a distance equal to the workpiece thickness plus the desired exit travel. For a blind hole, the Z-axis travels exactly to the programmed depth, and then retracts immediately—no extra distance needed. The machine’s control unit (most use Siemens or FANUC controllers, which we integrate into all our units) stores these depth settings, so you can save programs for different jobs and pull them up in seconds. That means if you switch from a job with all through-holes to one with all blind holes, you don’t have to reconfigure anything except selecting the new program.
Wait, but what about small holes, like for electronics? A lot of our clients make PCBs, right? Even the high-speed CNC drilling machines used for PCB fabrication do both through-holes (for vias that connect layers) and blind vias (that only connect two layers, stopping short of the bottom). That’s a perfect example of how even very small, precise holes rely on CNC drilling technology to switch between through and blind on the same job. We supply high-speed, small-spindle CNC drilling machines for PCB manufacturers, and they drill tens of thousands of holes per hour, both through and blind, with depth tolerances of less than 0.0001 inches. So that’s not just for big metal parts—it’s for tiny, precision parts too.
The only real catch, and the part I always emphasize to clients, is that success depends on two things: proper programming and proper setup. A CNC drilling machine is only as good as the person writing the program and setting up the tooling. If you write a program that sets a blind hole to drill all the way through because you confused the depth setting, you’ll ruin a part. If you use a dull drill bit for blind holes, you’ll get uneven bottoms. But that’s not a limitation of the machine—that’s a matter of operator training, which we provide for all our clients, along with free software updates to make programming through and blind holes even easier.
Let’s circle back to the original question: Can a CNC drilling machine be used for both through-hole and blind-hole drilling? After 10 years of selling, installing, and troubleshooting these machines, my answer is a resounding yes—but only if you choose the right CNC drilling machine for your needs, and understand how to adjust your programs and tooling for each hole type. The days when you needed separate machines for each are long gone; modern CNC drilling lines are built to handle both, and that’s one of the biggest advantages they offer over older manual or semi-automated drill presses.
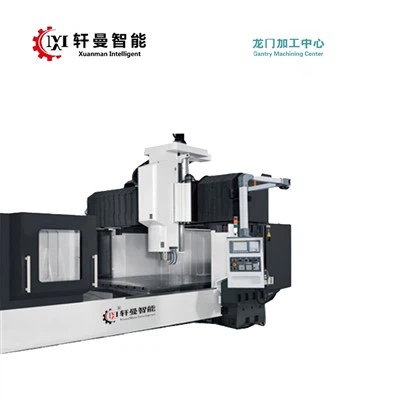
If you’re a production manager, machinist, or business owner looking to upgrade your hole-making process, and you’re wondering if a CNC drilling machine can handle both the through and blind hole jobs on your to-do list, we can help. We’ve worked with businesses of all sizes, from small job shops to large aerospace and automotive manufacturers, to find the right CNC drilling machine that fits their production volume, part types, and hole requirements. We don’t just sell equipment—we provide training, ongoing support, and custom program development to make sure you get the most out of your machine, whether you’re running a batch of 100 parts or 100,000 parts. If you’re ready to stop dealing with high scrap rates, inconsistent hole quality, and slow production times from outdated drilling equipment, reach out to our team to discuss your needs and find the perfect CNC drilling machine for your business.
CNC Drilling Machine References
- ISO 10360-7:2018, Geometrical product specifications (GPS) — Acceptance and reverification tests for coordinate measuring machines (CMM) — Part 7: CMMs used for measuring machined holes
- Smith, G. T., Cutting Technology: Principles and Practice, 3rd ed., Industrial Press, 2020
- DeVries, W. R., Analysis of Material Removal Processes, Springer, 1992
- Haas CNC Systems, “CNC Drilling Basics: Through-Hole vs. Blind-Hole Programming,” Technical Bulletin, 2022
- Aerospace Industries Association, “Precision Drilling for Aerospace Components,” Manufacturing Standards Report, 2021
Jiangsu Xuanman Intelligent Equipment Co., Ltd.
We’re well-known as one of the leading CNC drilling machine manufacturers in China, featured by quality products and low price. Please rest assured to buy discount CNC drilling machine made in China here from our factory. We also accept customized orders.
Address: No. 1-1, Weier Road, Jieji Equipment Manufacturing Industrial Park, Sihong County, Suqian City, Jiangsu Province, China
E-mail: jsxmzn@163.com
WebSite: https://www.xm-cnc.com/
