If you’ve ever watched a steel nut thread perfectly into a bolt, turning a slightly rough blank into a fastener with uniform, precise ridges that lock reliably every time, you might not have stopped to ask how that thread gets there. As a supplier of nut and bolt manufacturing machines, I get this question all the time—usually from new customers who are setting up their first production line or veteran operators troubleshooting inconsistent thread quality. Threading is the make-or-break step in fastener manufacturing; skip it, and your parts are little more than plain rods and round discs. Get it right, and you’ve got a component that works for automotive assemblies, construction, aerospace, and everything in between. Let’s break down how it works in modern nut and bolt manufacturing machines, with real-world insight from 12 years of designing, selling, and servicing these machines for workshops large and small. Nut Bolt Manufacturing Machine
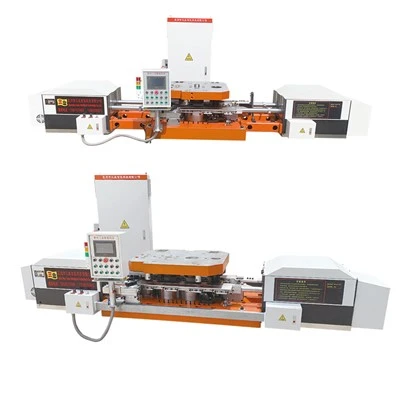
First, let’s clarify a simple fact: threading isn’t a single process. Different machine lines are built for different fasteners, so their threading mechanisms change to match. A M6 bolt used in furniture construction has different requirements than a heavy-duty M30 bolt for bridge steel, and hex nuts for plumbing need a different approach than wing nuts for machinery access. The core purpose is always the same: cut, form, or roll a continuous spiral ridge (male, on bolts) and matching spiral groove (female, on nuts) along the length of the fastener, with consistent pitch (distance between adjacent threads), diameter, and profile that meets industry standards like ISO, ASME, or DIN.
Let’s start with the two main categories of threading mechanisms in our machines: cutting threading and thread rolling. Most new workshops I work with lean toward thread rolling for high-volume production, while smaller setups or specialty fastener jobs often use cutting threading. Each has its own tools, pros, and best uses—something I always walk through with customers during our first consultation.
Let’s cover thread rolling first, since it’s the most common in automated, high-speed nut and bolt lines. Unlike cutting, which removes material from a pre-formed blank, thread rolling shapes the metal without cutting. That might sound counterintuitive, but it’s a game-changer for fastener strength. Here’s how it works step by step in our automated rolling machines:
First, the fastener blank comes from the heading machine, which cuts steel wire into individual blanks and shapes them into rough bolts or nuts (for bolts, this means a head formed on one end; for nuts, a hexagonal shape). For rolling, the blanks are heated slightly (but not enough to melt) in a heating chamber—usually induction heating, since it’s fast and precise—just soft enough to deform under pressure, but not so soft that they bend out of shape. This step is critical; too little heat, and the metal cracks during rolling; too much, and it warps.
Next, the blanks are fed one at a time into the rolling mechanism. The core components here are two cylindrical rolling dies, mounted on parallel shafts, set a tiny distance wider than the blank’s core diameter (for bolts, that’s the shank diameter; for nuts, the diameter of the hexagonal blank’s hole). Each die has a reverse-threaded spiral pattern machined into its surface—so if one die has threads curving clockwise, the other has them curving counterclockwise.
The machine’s feed system pushes the blank between the two rotating dies. As the dies spin, they apply extreme, consistent pressure to the blank’s surface. The metal flows into the grooves between the die’s threads, forming the male or female thread as it’s shaped. The rotation of the dies pulls the blank through at a steady speed, which ensures the pitch is uniform across the entire length. For bolts, the shank is fully rolled in a matter of seconds; for nuts, the hole in the hexagonal blank is aligned with the dies, and the same rolling process cuts the internal threads.
What makes our rolling machines stand out (and what I always highlight for customers worried about quality) is the precision of the die alignment and pressure control. If the dies are even a fraction of a millimeter out of line, you’ll get cross-threading, or threads that are too shallow on one side. Our machines use laser alignment sensors to calibrate die positioning before every run, and hydraulic pressure regulators that adjust in real time if the blank diameter varies slightly—something that’s become more important as we work with customers using recycled steel wire, which can have minor size fluctuations.
Now, the big advantage of thread rolling that sells most customers on it: it produces stronger threads than cutting. When you cut threads, you remove material, which disrupts the metal’s grain structure—think of bending a stick at a weak point where you’d nicked it earlier. Rolling compresses the metal’s grain along the thread’s shape, making it denser and more resistant to shear stress. That’s why rolling threads is the industry standard for most high-load fasteners, from automotive engine bolts to construction anchor bolts. The only time cutting threading is preferred is for specialty jobs: very small fasteners that would be too delicate for rolling, or custom profiles that can’t be machined into rolling dies.
Cutting threading, sometimes called thread cutting or die threading, is the other main mechanism, and it’s been around longer than rolling—though modern versions are far more precise than the manual dies your grandfather might have used in a workshop. There are two common types of cutting threading in our machines: single-point cutting and tap and die threading.
Let’s start with tap and die threading, which is the most common for medium-volume jobs. For bolts, a rotating die (a cylindrical tool with sharp, helical cutting edges matching the desired thread profile) is fed along the blank’s shank. The blank is held in a fixed chuck, and the die spins while advancing at exactly the same speed as the thread’s pitch—so each full rotation of the die moves forward by one pitch unit, creating a continuous, uniform cut. For nuts, the process is reversed: a rotating tap is inserted into the pre-drilled hole of the hexagonal blank, cutting the internal threads as it spins in the reverse direction of the bolt die.
Single-point cutting is a bit more specialized, used for custom fasteners or jobs where the thread profile isn’t standard. Instead of a die or tap, the machine uses a sharp, moveable cutting tool (usually a carbide insert, since it needs to stay sharp through thousands of cuts) that cuts a single thread groove at a time. The tool moves along the blank’s length in line with the pitch, cutting the spiral profile gradually. This method is more flexible than die threading, but it’s slower and can produce slightly rougher threads, so it’s mostly used for low-volume, specialty runs.
I’ve had customers come to me confused about when to use which method, and I always walk them through their production goals. If you’re making 10,000 M8 bolts a day for furniture parts, thread rolling is cheaper, faster, and produces stronger parts. If you’re making 500 custom M12 bolts with a non-standard thread profile for a small construction project, cutting threading is the way to go. There are exceptions, of course—some aerospace manufacturers still use cutting for very fine threads that need extremely tight tolerance, but those are far fewer than they used to be, thanks to advances in die manufacturing.
One key part of any threading mechanism that I don’t see mentioned enough is the quality control step that’s built into modern machines. A few years ago, we sold a line of bolt manufacturing machines to a small automotive parts supplier, and within a month, they were calling complaining about 2% of their bolts cross-threading. I flew out to their workshop to look at the machine, and it turned out their old machine’s die alignment sensors had been broken, so they were running off-spec dies. We upgraded their machine to our new real-time thread inspection system, which uses a laser scanner to check the thread profile as the part comes off the line, immediately rejecting any parts that have too shallow a thread, uneven pitch, or cross-threading. That’s a huge upgrade from older machines that required manual inspection, which is slow and error-prone.
Another common question I get is about wear and maintenance, which is the biggest cost for any fastener manufacturer. Threading dies—whether for rolling or cutting—wear out over time, especially if you’re running high volumes on hard steel. Rolling dies can last 200,000 to 500,000 parts with regular maintenance (cleaning and reconditioning the die surface), while cutting dies might last 50,000 to 100,000 parts before they need to be replaced. Our machines come with a die wear monitoring system that tracks how much the die’s profile has shifted, alerting operators when it’s time to recondition or replace the die, so they don’t have to stop production unexpectedly.
I’ve also worked with customers who make small specialty fasteners, like wing nuts or rivet nuts, which have a slightly different threading challenge. For wing nuts, the threading mechanism has to accommodate the two wing arms, so the machine aligns the hexagonal blank between the dies, rather than the head of the bolt. For rivet nuts, which are used to fasten parts from the inside of a hole, the internal thread is rolled from a hollow cylindrical blank, so the dies have to align precisely with the hollow center to avoid damaging the edges of the hole. We designed a custom adapter for our rolling machines specifically for rivet nuts a few years back, and it’s become one of our most popular add-ons for small workshops that do a lot of automotive repair parts.
Let’s talk about a common misconception I hear all the time: that cheaper, imported machines work just as well for threading. I’ve seen too many customers buy a budget machine from overseas, only to have to replace their dies every 50,000 parts, or deal with inconsistent thread quality that leads to rejections. The precision of the die manufacturing, the alignment sensors, and the control software that regulates die speed and pressure makes a huge difference in thread consistency. Last year, a customer switched from a $80,000 imported bolt line to our $120,000 line, and they cut their rejections from 4% to less than 0.5%, and increased their production rate by 15%—that’s a huge return on investment, even with the higher upfront cost.
If you’re running a nut and bolt manufacturing operation, the threading mechanism isn’t just a step in the process—it’s the core of your product quality. A fastener with poorly formed threads won’t hold up, no matter how well the head is shaped or the blank is cut. That’s why when we design our machines, we spend more time on the threading module than any other part: calibrating die alignment, integrating real-time inspection, and building systems that minimize wear and downtime.
Whether you’re setting up your first production line and trying to decide between rolling and cutting, or you’re looking to upgrade an older machine to reduce rejections, there’s no one-size-fits-all answer. The right threading mechanism depends on your production volume, the type of fasteners you make, and your quality requirements. If you’re ready to talk through your specific needs, or you have questions about how our machines’ threading systems work, feel free to reach out to connect with our team for a consultation. We’re here to help you find the right solution, not just sell you a machine.
Busher Former Machine REFERENCES
- Kalpakjian, S., & Schmid, S. R. (2020). Manufacturing Processes for Engineering Materials. Pearson Education.
- Degarmo, E. P., Black, J. T., & Kohser, R. A. (2018). Materials and Processes in Manufacturing. John Wiley & Sons.
- Thread Rolling vs. Thread Cutting: A Comparative Analysis for Fastener Manufacturers. Fastener Technology International, 2021.
- ISO 898-1: Mechanical Properties of Fasteners Made of Carbon Steel and Alloy Steel, 2013.
Quanzhou Sanye Intelligent Technology Co., Ltd.
As one of the most professional nut bolt manufacturing machine manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy customized nut bolt manufacturing machine made in China here from our factory. Welcome to contact us for quotation.
Address: Anhai Town, Jinjiang City, Fujian Province, China
E-mail: jack_tmm@163.com
WebSite: https://www.qzsymanipulator.com/
