If you’ve ever worked with advanced ceramics, technical refractories, or even some specialized cement products, you know high temperature tunnel kilns aren’t just big metal boxes that heat stuff up. They’re carefully tuned systems, and the pre-heating zone is arguably the unsung hero of the whole operation. As someone who’s spent the last decade designing, building, and troubleshooting these kilns for clients across heavy industry, I can tell you: skip getting this zone right, and you’re gonna have way more cracks, energy waste, and failed batches than you bargained for. Let’s break this down like I would over a coffee at a trade show, no stuffy jargon just real-world stuff. High Temperature Tunnel Kiln
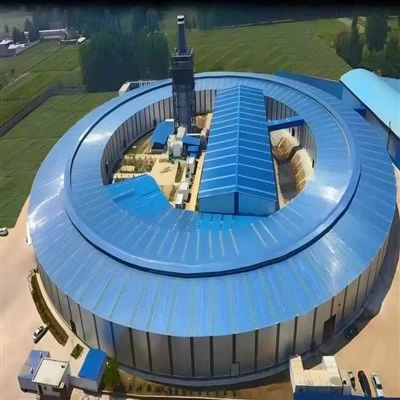
First off, let’s ground this in what a tunnel kiln actually does. It’s a continuous system—ware-like, usually lined with heavy-duty refractory bricks, that pushes kiln cars (or sometimes batches of product) through different temperature zones on a rail line. You’ve got your pre-heating zone, then your high-temperature firing zone, then a cooling zone at the end. Most people fixate on the firing zone, right? That’s where the product hits 1,200°C, 1,800°C, even higher for super specialized materials, and that’s where the chemical “magic” happens—like sintering ceramic particles or bonding refractory minerals. But if you yank your cold product straight into that 1,700°C firing zone? Bad news. Like, immediate stress bad.
That’s where the pre-heating zone steps in. Its main job is to warm your product up gradually, no sudden temperature spikes, so the internal structure of whatever you’re firing can adjust slowly. Let’s take a common example: alumina ceramic insulators for electrical equipment. Those are dense, slightly porous greenware right out of the press—cold, full of residual moisture, and if you blast them with 1,500°C right away, the water inside would turn to steam way too fast, create internal pressure, and blow cracks in the insulator. Not good, especially when they’re supposed to stop current. The pre-heating zone is where that steam escapes slowly, over hours as the kiln car inches along, so you don’t get explosive failures before you even hit the firing zone.
Wait, it’s not just moisture, though. Most materials have volatile compounds too—binders, organic lubricants, even leftover processing chemicals from shaping. Greenware (unfired product) isn’t just clay or ceramic powder; it’s mixed with stuff to make it moldable, stuff that burns off before the high firing stage. If those volatiles don’t get a controlled path to escape, they can get trapped inside the product, cause blisters, or even leave tiny voids that weaken the finished part. The pre-heating zone is temperature-locked specifically for this: usually 200°C to 800°C, depending on the product. That’s exactly the range where binders and processing aids break down without combusting too violently. We’ve had a client making silicon carbide kiln shelves tell us before that before they upgraded their pre-heating zone, they were scrapping 12% of their shelves because of blisters and voids. Once we adjusted the zone’s air flow and temperature ramp to match their binder, that scrap rate dropped to less than 2%—straight from getting the pre-heating zone right.
Another big role people sleep on: energy efficiency. Let’s be real, high temperature kilns use insane amounts of fuel—some of our big units run on natural gas or even electricity at rates that make small factory owners wince. The pre-heating zone works in tandem with the cooling zone to recapture that heat, instead of wasting it up the stack. Think about it: the cooling zone is where you pull your hot fired product from 1,700°C down to room temp, and all that heat it’s releasing would just float out the stack if you don’t redirect it. So we design the pre-heating zone to pull that waste heat from the cooling zone, so you’re not having to burn extra fuel just to heat cold product from ambient temp up to firing temp. Before we added that heat recovery loop to a refractory manufacturer’s kiln, their monthly gas bill was $42,000. After? It dropped to $28,000. That’s not pocket change—they were able to pass some of that savings to their clients and still grow their profit margin. And for anyone worried about carbon footprints? That’s a huge win for sustainability too, which is a big deal these days for all kinds of industrial clients.
Wait, let’s get specific about how we structure the pre-heating zone, since that’s the part that makes it actually work, not just a random warm part of the kiln. It’s not just one long chamber—we split it into smaller, incremental temperature stages, usually 200°C, 400°C, 600°C, 800°C, so each step is only a 100-200°C jump every time the kiln car moves. That gradual ramp is key for reducing thermal stress. Thermal stress is when different parts of a material heat up at different rates—like the outside warming up fast and the inside staying cold, which causes expansion that cracks the material. We also control air flow in the pre-heating zone: we pull air (with the volatile fumes) out at specific points, not all at once, so we don’t suck too much heat out too fast, and we filter those fumes before they go out the stack—another win for emissions.
Let’s talk about what happens if you mess up the pre-heating zone, because that’s the stuff we see every day as kiln suppliers. I had a client last year who bought a used tunnel kiln on the cheap, and the previous owner had basically patched over the pre-heating zone with extra refractory bricks, because they thought it was a waste of space. They were firing cordierite honeycombs for diesel exhaust filters, and their first batch had 30% scrappage—all from cracks, blisters, and warped parts. We went in, measured the temperature profile, and found that their “pre-heating zone” only hit a max of 300°C, so the cordierite was going straight from room temp to 1,200°C firing zone, with nowhere for the moisture and binders to go. We retrofitted the zone, added the incremental temperature stages, adjusted the air flow and heat recovery, and their scrap rate went down to 4% within a month. That’s not just fixing a part of a kiln— that’s saving a company tens of thousands of dollars a quarter.
Another example: we work with some aerospace clients that fire high-purity alumina components for jet engine parts. Those parts have to be 100% dense and free of any impurities, right? The pre-heating zone’s temperature control is critical here. If it’s too cold, the binders don’t burn off completely, leaving carbon residue that ruins the purity. If it’s too hot too fast, the alumina starts sintering unevenly, leading to weak spots in the final part. We’ve fine-tuned the pre-heating zone for these clients to ramp at 150°C per hour, with oxygen levels monitored the whole time, so the binders burn off completely without oxidation of the alumina. The result? Parts that meet aerospace standards on the first try, no rework.
Wait, I should also clarify that the pre-heating zone isn’t one-size-fits-all. We design it based on the product you’re firing, because different materials have totally different needs. A delicate ceramic filter for water treatment needs a slower, lower-temperature ramp than a dense silicon carbide refractory for steel mills. A batch of porcelain dinnerware? Even different pre-heating than electrical insulators. That’s why we don’t sell “generic” kilns—we talk to clients about their product first, then size and design the pre-heating zone to match their specific material’s thermal and chemical requirements. That’s the stuff that makes our kilns different from the cheap imports some clients try to save money on—we don’t skip the pre-heating zone to cut costs, because we know it’s the difference between a good batch and a bad one.
Let’s circle back to energy, because that’s a big pain point for almost every industrial kiln user. The pre-heating zone is the bridge between the cooling zone (where waste heat is generated) and the firing zone (where you need intense heat). Without it, all that heat from the cooling zone is lost, and you have to produce all the heat for the pre-heating zone separately from the firing zone. With a properly designed pre-heating zone, we can recapture up to 60% of the waste heat from the cooling zone, and redirect it to warm the product up before it hits the firing zone. That translates to less fuel burned, lower energy bills, and fewer emissions—all while improving product quality. It’s a win-win-win, honestly.
I’ve seen so many kiln projects go sideways because the pre-heating zone was an afterthought. A client a couple years back hired a contractor who cut corners on the zone to save on build time, and their kiln could never hit the consistent temperature required for their product—they had to shut down operations for two months to redo the pre-heating zone, costing them hundreds of thousands in lost revenue. That’s why when we work with new clients, we spend the first couple of meetings walking through their production process, their product specs, their energy goals, and design the entire kiln system around the pre-heating zone, not the other way around. Because at the end of the day, a kiln is only as good as its weakest zone, and the pre-heating zone is almost never the one you want to be weak.
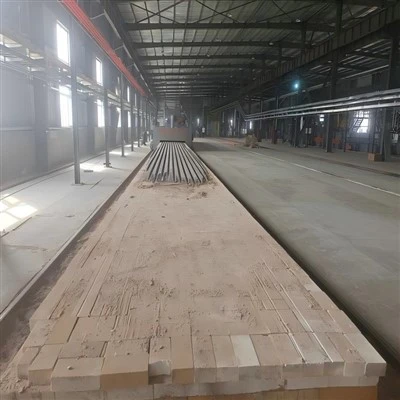
If you’re in the market for a new high temperature tunnel kiln, or you’re looking to upgrade an existing one to fix scrap rates or lower energy costs, don’t just ask about the firing zone. Ask about the pre-heating zone: how is it designed? Is it tailored to your product? Does it have heat recovery from the cooling zone? Those are the details that make a kiln work, not just the big hot part in the middle. We’ve helped dozens of clients fix kilns that were underperforming because their pre-heating zone was wrong, and we’d be happy to sit down and walk through what we can do for your operation. Just reach out—we’ll give you a real, no-flat answer, not a sales pitch, and work with you to build a kiln that fits your exact needs.
Ceramic Tunnel Kiln References
- Carter, C. B., & Norton, M. G. (2007). Ceramic Materials: Science and Engineering. Springer.
- Hlavac, J. (1995). Tunnel Kilns: Design and Operation. Industrial Press Inc.
- Perera, D. S. (2001). Thermal Stress in Ceramics and Refractories. Journal of the European Ceramic Society.
- World Bank Group. (2020). Industrial Energy Efficiency Improvement for Heavy Industry.
Henan Yaxin Kiln Co., Ltd.
Henan Yaxin Kiln Co., Ltd. is one of the most professional high temperature tunnel kiln manufacturers and suppliers in China. With abundant experience, we warmly welcome you to buy high quality high temperature tunnel kiln with the latest design from our factory. Good service and punctual delivery are available.
Address: Jixian Industrial Zone, Shangqiu City, Henan Province
E-mail: 1543563178@qq.com
WebSite: https://www.hnyxkiln.com/
